When you move a plastic part from CAD to physical samples, one question decides your budget, timeline, and risk:
Do you need rapid tooling or production tooling?
Both use the same injection molding process. The difference is the tooling strategy — how the mold is built, how long it lasts, and what stage of your product lifecycle it supports.
At Danke Mold, we build both. We don’t push one option because it’s more expensive. We help you match the mold to your stage, so you don’t overpay for a production tool too early — or outgrow a rapid tool too fast.
What Is Rapid Tooling?
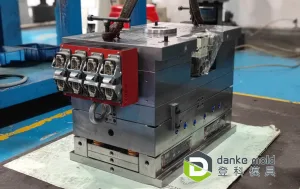
Rapid tooling (also called prototype tooling or bridge tooling) is a simplified mold built for speed and flexibility.
Typical construction:
- Pre-hardened steel (P20, NAK80) or Aluminum 7075.
- Standard mold base with removable inserts
- Single-cavity or low-cavitation layout
- Simplified cooling and ejection
- No full heat treatment cycle
Lead time: as fast as 14 days for T1 samples
Tool life: typically 500 – 50,000 shots, depending on resin and geometry
Best for: design validation, pilot runs, crowdfunding fulfillment, bridge production, low-volume orders
Rapid tooling is not “worse quality.” You still get real injection-molded parts in your production resin — with real shrinkage, weld lines, snap-fit behavior, and surface finish. The trade-off is mold durability, not part accuracy at low volume.
What Is Production Tooling?
Production tooling is a hardened steel mold engineered for long-term, high-volume manufacturing.
Typical construction:
- Hardened tool steel (H13, S7, 420SS)
- Multi-cavity or family-mold layouts
- Engineered cooling, hot runners, automation-ready ejection
- Tight tolerances and repeatable process control
Lead time: usually 8–20 weeks
Tool life: 500,000 to 1,000,000+ shots
Best for: stable designs, automotive/medical-grade programs, annual volumes in the tens or hundreds of thousands
Production tooling costs more upfront — but the per-part cost drops sharply once volume absorbs the tooling investment.
Rapid Tooling vs Production Tooling: Side-by-Side
| Factor | Rapid Tooling | Production Tooling |
| Mold material | Aluminum / soft steel | Hardened tool steel |
| Lead time | 2–6 weeks (14 days possible) | 8–20 weeks |
| Upfront cost | Lower | Higher |
| Tool life | Hundreds to tens of thousands of shots | 500k–1M+ shots |
| Cavitation | Usually 1 cavity | Multi-cavity / hot runner |
| Design changes | Fast & affordable | Slow & costly after hardening |
| Per-part cost | Higher at scale | Lower at volume |
| Best use | Prototyping, bridge, low-volume | Mass production |
Ranges are planning references. Actual cost and life depend on part size, resin, tolerance, surface finish, and cavitation.
When to Choose Rapid Tooling
Choose rapid tooling if:
- Your design is not 100% frozen yet
- You need functional samples in production material for testing
- You’re running a pilot batch of 50–10,000 parts
- You want to launch at a trade show or validate market demand
- Your production mold is still being built and you need parts now
- You have no MOQ and don’t want to commit to 100k units yet
Example: an EV charger housing in PC+ABS. Before locking a $40k production mold, our client ran a rapid tool for functional samples and early low-volume sales — then transitioned to hardened tooling only after the design was proven.
When to Choose Production Tooling
Choose production tooling if:
- Your design is released and stable
- You need 50k+ parts per year
- You run glass-filled, corrosive, or high-temp resins
- You need tight, repeatable tolerances over the full program
- You require automation, multi-cavity output, or SPI-A1 polish
- You need documented process control (FAI, CoC, SOP, PPAP-style records)
If your resin is 30% glass-filled nylon, aluminum rapid tooling will wear quickly. You’ll want P20 at minimum, and hardened steel for long runs.
The Smart Path: Rapid First, Then Production
Most mature hardware programs don’t pick one or the other. They use both — in sequence.
- Rapid tooling → validate fit, function, mold flow, assembly, and market response
- Parallel engineering → start production tool design while rapid parts ship
- Production tooling → scale up with locked drawings and real molding data
This hybrid approach protects your schedule. You don’t wait 4 months to discover a draft angle was wrong.
How Danke Mold Helps You Decide
We’ve been building custom injection molds and rapid tools for 12+ years for clients in the US, UK, Germany, and across Europe.
When you send us your 3D files, we don’t just quote blindly. We review:
- Wall thickness, draft, ribs, bosses, undercuts
- Gate location and fill balance
- Resin shrinkage and wear on the mold
- Tolerance risk and cosmetic requirements
- Whether rapid or production tooling is the better ROI
Every quote includes free DFM analysis — so you know the right tooling path before cutting steel.
Why buyers work with Danke Mold
- ✅ Free DFM feedback with every quote
- ✅ Rapid tooling with T1 samples as fast as 14 days
- ✅ No MOQ — from 50 parts to full production
- ✅ 《ISO 9001:2015》 quality system, CoC + FAI reports
- ✅ Fluent English communication (email, video call, weekly updates)
- ✅ Real engineering support, not just sales talk
We tell you honestly when a rapid tool is enough — and when you’d be wasting money not building production tooling.
Get the Right Mold the First Time
Choosing between rapid tooling and production tooling isn’t about which is “better.” It’s about where your product is today.
Send us your STEP/IGES files, target quantity, resin, and surface finish. We’ll return a quote plus a clear tooling recommendation — backed by DFM, engineering logic, and 16+ years of mold-making experience.
👉 Request a Quote at www.dankemold.com
Free DFM analysis • English-speaking engineers • Rapid tooling & custom injection molding from prototype to production.